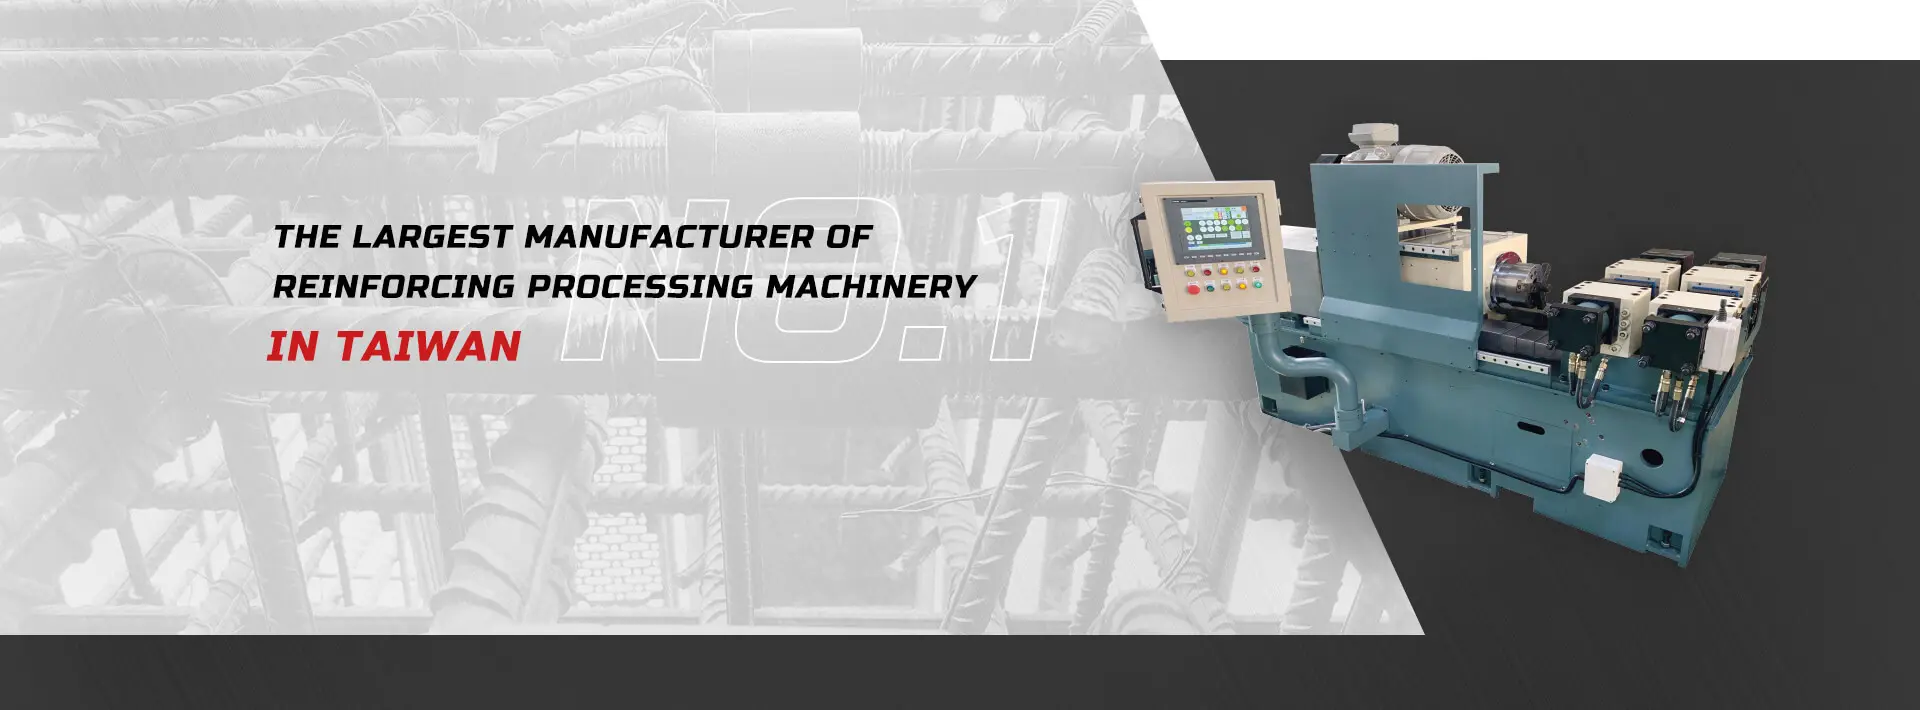

DH-FW45 Rebar Friction Welding Machine
The invention is a "Rebar Friction Welding Machine with Servo Mechanism", which uses a servo motor to turn a screw and converts the traditional hydraulic pressure of the welding process to digital information that can be accurately recorded. The invention provides innovative means for producing quality-coupled rebar by friction welding so the structure of the building is more stable than government safety requirements. All the associated work experience based human errors appear to be eliminated, which makes it very cost effective solution. After the data has been verified and input, this machine assures that the machine runs smoothly throughout the production process and shows the effectiveness of rebar friction welding, friction welding machine, and rebar welding service.
- Description
- A solid-state welding procedure utilises both mechanical friction along with axial pressure to create heat at the surfaces being welded. The material is in a semi-molten state which allows for a good solid weld to occur once the pressure is applied to the two work pieces being joined together. Friction Welding can be used to weld same metals together or different types of metals together as one single piece.
- Conserving energy will be a critical aspect of achieving a low-carbon society through welding. If you lessen the amount of heat that you use, you will not produce as much spatter as well as smoke at the point of joining. You will therefore not have to use any additional materials and/or fillers in this application. What you are doing is changing the very nature of how you fabricate your products.
- Friction welding has been a Well-Tested Technique in the Construction Industry of Taiwan for more than Thirty years. The basic process consists of three events, i.e. Heat up and Pressing Forces (i.e. Standard and Forging Pressures). By using two Hydraulically Driven cylinders as pushers, variation in the Oil Temperature is seen to occur which causes an overall significant Decrease in the Friction Welding Success Rate.
- Friction Welding has served the construction industry well for many years. "Friction Welding Machine With Servo Mechanism" (Patented) uses a Screw With Servo Motor To execute The Functions Performed By Hydraulic Pressure Traditionally In Friction Welding Machines, Such Pressure Values Are Also Represented Digitally". This advancement enables the manufacturing of quality re-bars that are properly coupled together to improve the overall strength of a structure, and also exceeds government safety standards. Our technology eliminates all of the mistakes that a new worker could do. The machine will automatically perform all of the steps after the data has been validated.
- We're using the newest type of servo drive in our friction welding machine, to make welding rebar faster, more accurate, and more efficient.The full touch panel offers enhanced flexibility, adaptability, and a high degree of freedom. It can be equipped with a cutting device and driving pushing structure supported by an automatic cutting waste servo motor. Utilizing friction welding in the production process ensures numerous benefits, including heightened process efficiency, increased productivity, excellent joint properties, and safe working conditions.
- Friction welding offers a cost advantage in coupler production over forging, with the added benefit of swift formation. The strength of friction-welded products equals that of their forged counterparts, and the resulting surface is noticeably cleaner.
- SpecificationAutomatic Friction Welding Machine
ITEMMODEL
DH-FW-45
Spindle Speed (RPM)
1800 RPM Max. Material size on spindle side (mm.)
Ø40*200L Main Spindle Motor
40HP Servo motor-Max. Thrust (TON)
23TON Welding capacity diameter range
Ø16- Ø40 Cooling model
Oil cooling Clutch
Wet multiple magnetic clutch Brake device
Wet multiple magnetic brake Braking time 0.2sec Control system Touch panel Welding material
Aluminum,Iron,Steel,Copper,Stainless steel,Steel bar - Video
- Principle
Unique welding function
By attaching the two ends of the metal together by melting the meeting surface. creates a very tough bond. This bond can handle more pulling and twisting than can be achieved through the use of arcwelding or argonwelding.
Dissimilar materials can be added to reduce overall material cost
Friction welding is a technique for connecting various metals, that cannot otherwise be welded with traditional methods. Thisnot onlycrsavecostandbutisagood alternative methodofcreatingLightweightComponentApplicationaswellin
More accurate weldingThe materials of the two ends have almost no deformation after welding, and the distance between the centers of the materials is 0.5m/m, which is an important commitment quality workpiece that can reduce the machining allowance and also reduce the material cost and processing cost.
Eco-friendly, Energy-efficient processes
The materials and fillers, such as metals, fluxes and gases etc., are not consumed during the welding process. There is also no arc or toxic products produced, which makes it much safer and better in the overall environment.
Faster and more accurate welding efficiency.
Production costs are lower when you make a product with friction welding compared to forging. The process also results in faster formation time than forging. The finished product is basically as strong as a forged piece and has a much cleaner surface.
Operator error is eliminated.
Because the friction welding process is machine-controlled, it achieves uniformity and repeatability. There is no human error involved in this process. At the same time, quality of the weld created through machine friction welding is independent quality that exceeds the skill level of the operator.
- Features
a) When the integration of the welding surfaces occurs at the ends of the metal, the weld possesses a strong & durable joint. Therefore the tensile strengths, as well as, torsional strengths of the result weld are much greater than that produced by arc or argon welding methods.
b. A lot of different types of materials can be joined through welding process i.e. stainless steel with many types of medium carbon steels and high carbon steels, however, high carbon steel must be annealed after welding. In the post-welded conditions, both ends of the materials are almost the same (no offsets) and the center has an eccentricity difference of less than 0.5 mm, which is functional for the quality of the work piece, saving the quantity of material used and the cost of processing.
c. Friction welding allows for the speedy creation of parts at a lower cost than forging, yet is similar to forged materials in strength, with an improved surface quality upon welding completion.
d. When compared to arc welding, friction welding uses no expendable materials (fuel, gaseous, metallic or otherwise-filled solvent, etc.), therefore producing a safe and non-toxic work area. The heat created in the process of friction welding is produced indirectly through friction at the interface of the materials being welded. - Optional1.Optical scale positioning module
-Easy and fast operation, precise length adjustment
-Detectable work piece lengthOptical scale positioning module2.Rotary angle positioning
-both ends of the work piece after welding can be stopped at certain angles3. Inverter
-Adjustable spindle speed
-Save spindle start energy consumption
-Extended service lifeInverter4.Chip system
-Increased chip system
-Servo Motor Chips (Simple PLC Control or CNC Program Control)
Chip system5.Electric control box cooling system
- Standard original fan
- Upgradeable the heat exchanger or air conditioner.
Electric control box cooling system6.Safety Light buzzer
- Protecting the operators safety.7.Mechanical full cover safety guard8.Bar Conveyor9. Coulpers clamping robot - Advantages of servo control
Achieving stable operation without being influenced by oil temperature fluctuations, our system enables high-precision welding. Angle control further broadens the applications of friction welding, extending to phase-adjusting workpieces. The implementation of servo control not only enhances energy efficiency but also reduces carbon dioxide emissions compared to hydraulic control, making it an eco-friendly option. With no oil leakage, the working environment is improved, and the absence of waste oil contributes to environmental preservation. The feedback control of forge force ensures smooth operation at low speeds, and the downsized hydraulic unit results in space-saving and reduced noise.
Main Advantages of Friction Welding Machine.
The newest servo drive offers improved accuracy during transitions. You can easily control how the machine moves, with the option to change the speed at which it moves. There’s also no chance of an inconsistent oil temperature being maintained, which reduces negative impacts on the machine's performance. It is designed with a full touch screen control panel, that can be moved anywhere and by any means, and allows users total control of the machine. You can add a cutting tool to the machine, to automate the cutting of the waste material. The machine has been built with high-quality components from well-known manufacturers in different parts of the world, which ensures that the machine produces high-quality parts. Shaping speed is 5 times faster than in all previous machines. The automated system allows you to produce more parts with fewer labourers and less labour time.
- DH-FW Specification form
Machine specifications
DH-FW30
DH-FW45
DH-FW60
welding ability
Round rod diameter
Ø9 ~ Ø25 Ø15 ~ Ø36 Ø20 ~ Ø60 Pipe Fittings
Ø16 Ø48.3 Ø88.9 The Max. length of the rotating side
300 mm 300 mm 300 mm The length of the fixed side
9m 9m 9m Maximum thrust
Frictional heating time
8,000 Kg 10,000 Kg 12,000 Kg Forging pressurization
16,000 Kg 20,000 Kg 26,000 Kg Spindle
Number of spindle rotation (50Hz)
3000 rpm 2250 rpm 1780 rpm Number of spindle rotation (60Hz)
2500 rpm 1780 rpm 1570 rpm Clutch Direction
Oil Actuated Multi-Disc Clutch and Brake Clutch Torque
800 (N.m) 800 (N.m) 1600 (N.m) brakes System Direction
Oil Actuated Multi-Disc Clutch and Brake brakes System Dynamic Torque
800 (N.m) 800 (N.m) 1600 (N.m) Brakinf Time
0.3 sec 0.3 sec 0.3 sec Spindle Fixture
Three-jaw 6”/(Hydraulic Pressure) Three-jaw 8”/(Hydraulic Pressure) Three-jaw 10”/(Hydraulic Pressure) Slide Speed
Rapid Traverse rate
20 m/min 20 m/min 20 m/min Machine Processing speed
1~1000 mm/min 1~1000 mm/min 1~1000 mm/min The Max. moving
150 mm 200 mm 250 mm work piece clamping manner
Vise splint method
Horizontal double-open synchronous fixture Clamping force
8,600 Kg 17,000 Kg 25,000 Kg Processing Methods
Size adjustment
0 ~ 100 mm 0 ~ 100 mm 0 ~ 100 mm Time adjustment
0 ~ 999 秒 0 ~ 999 秒 0 ~ 999 秒 Motor Power
Spindle
22 kw 30 kw 37 kw Hydraulic Pressure
5 kw 9 kw 9 kw Servo motors
7 kw 9 kw 11 kw Hydraulic Oil Temperature cooling system
1.5T / 1.1 Kw 2T / 2 Kw 2T / 2 Kw Dimension
Machine Dimensions
2750 x 2800 x 2000 2750 x 3100 x 2000 2750 x 3400 x 2000 Machine Weight
6,000 Kg 6,800 Kg 7,300 Kg
Related Products
DH-FW60 Rebar Friction Welding Machine